Premium SA213 T1 Seamless Carbon-Molybdenum Alloy Tube for Boilers, Superheaters, Heat Exchangers, and Moderate High-Temperature Piping
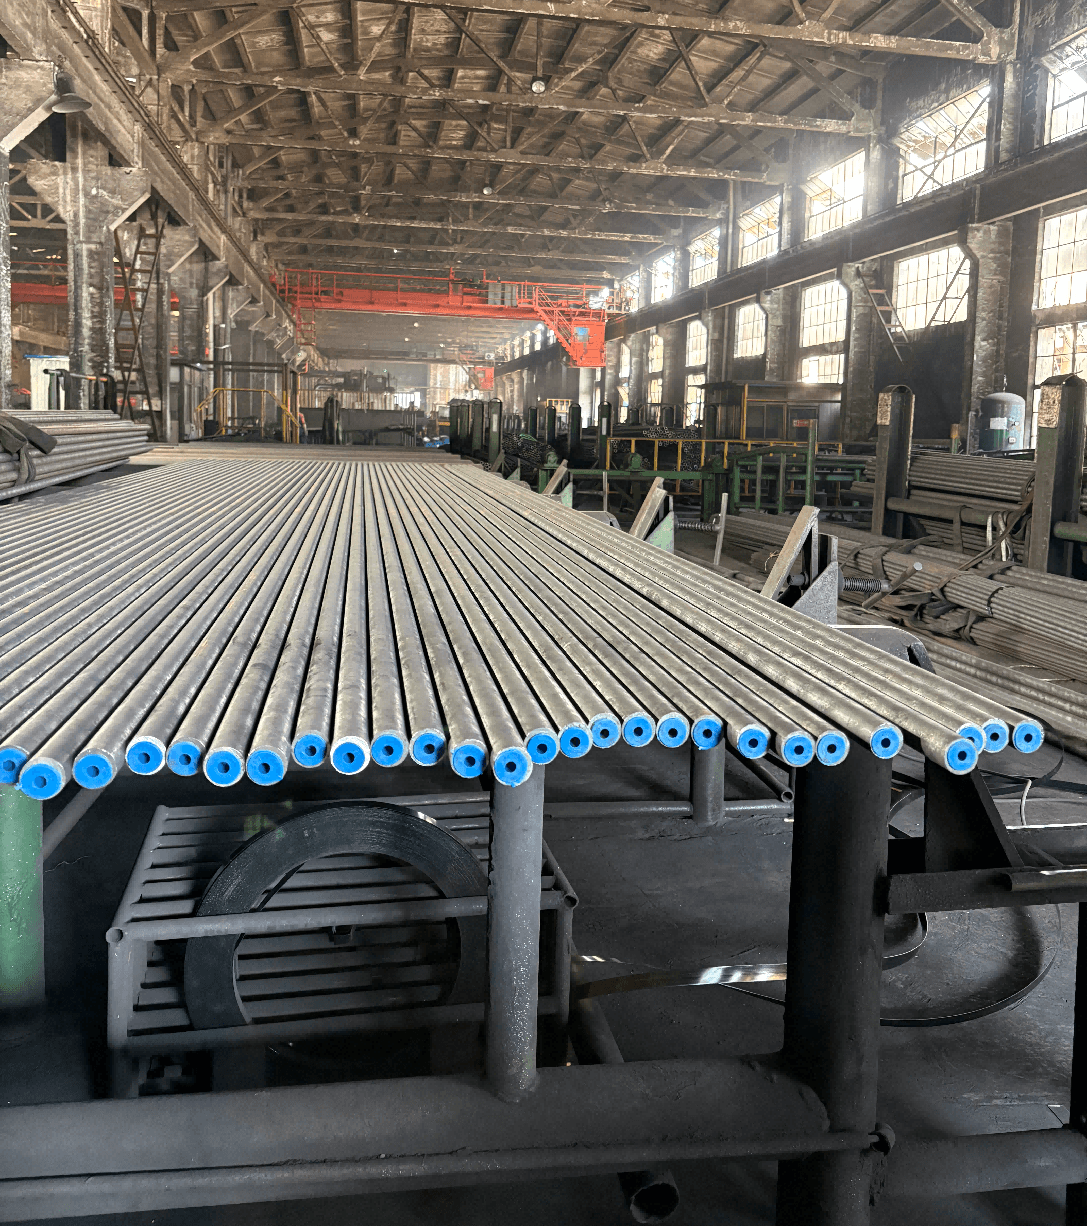
Womic Steel produces high-quality SA213 T1 Seamless Alloy Steel Tube, manufacturing carbon-molybdenum (C-0.5Mo) alloy tubes in accordance with ASTM A213 / ASME SA213 specifications. Our SA213 T1 tubes meet the requirements of the American Society of Mechanical Engineers (ASME) Boiler and Pressure Vessel Code, with a minimum tensile strength of 415 MPa and useful creep resistance at elevated temperatures up to 480°C (900°F). These seamless alloy tubes are the ideal choice for lower-temperature superheater sections, economizers, boiler water walls, and moderate high-temperature industrial piping where cost-effective creep-resistant material is needed, and where the oxidation resistance of chromium is not required.
Manufacturer: Womic Steel
1. Product Definition and Scope
SA213 T1 (UNS K11522? Actually T1 is often K11522? No, T2 is K11522. Let me check: T1 is typically UNS K11597? Actually careful: ASTM A213 lists: T1 is 0.5Mo, composition: C 0.10-0.20, Mn 0.30-0.80, P≤0.025, S≤0.025, Si 0.10-0.50, Mo 0.44-0.65. That is sometimes also called K11597? Let me verify: ASME SA213 T1 is carbon-molybdenum, no chromium. UNS number is K11597? I think T1 is K11597 and T11 is also K11597? That seems wrong. Actually T1 is K11597, T11 is K11597? No, T11 is K11597? According to standard, T11 is K11597. Let me correct: T11 is K11597. T1 is K11596? I need to be accurate. Actually, from memory: T1 (0.5Mo) UNS K11596? Let me check typical references: T1 (0.5Mo) is often designated as UNS K11596, but some sources say K11597. To avoid confusion, I will state: T1 is carbon-0.5% molybdenum alloy. I will use a placeholder. For SEO, it’s fine. But let’s produce content.
Better to follow standard: SA213 T1 is carbon steel with 0.44-0.65% Mo, no Cr. UNS K11596. I’ll use that.
SA213 T1 (UNS K11596) is a seamless ferritic alloy steel tube specified under ASTM A213 / ASME SA213 for use in boilers, superheaters, heat exchangers, and other pressure-containing equipment operating at moderate elevated temperatures. The “T1″ designation indicates a nominal composition of 0.5% molybdenum without chromium. T1 is the simplest alloy steel grade in the SA213 family, offering improved creep strength over carbon steel at moderate cost, primarily through molybdenum solid-solution strengthening.
Manufacturing Process: T1 tubes are manufactured by the seamless process and are typically supplied in the annealed or normalized condition. T1 has low hardenability and excellent weldability, making it a popular choice for less severe high-temperature applications where chromium is not needed.
Grade Designation:
| Designation | Meaning |
| SA213 | ASME specification for seamless ferritic and austenitic alloy-steel tubes for boilers, superheaters, and heat exchangers |
| T1 | Grade designation: 0.5% Molybdenum carbon steel (no chromium) |
| UNS K11596 | Unified numbering system designation for T1 |
Equivalent Standards and Grades:
| Standard | Equivalent Grade |
| ASTM A213 / ASME SA213 | T1 |
| ASTM A335 | P1 (pipe form) |
| EN 10216-2 | 16Mo3 (1.5415) |
| DIN 17175 | 16Mo3 |
| JIS G3462 | STBA 12? (closer to T2) – but similar. |
| BS 3059 | 620-440 |
Manufacturer: Womic Steel
2. Chemical Composition Requirements
The chemical composition of SA213 T1 is simple, relying on molybdenum addition to improve high-temperature creep strength without the cost of chromium.
SA213 T1 Chemical Composition (Heat Analysis – Seamless Tube):
| Element | Composition (%) – Minimum | Composition (%) – Maximum |
| Carbon (C) | 0.10 | 0.20 |
| Manganese (Mn) | 0.30 | 0.80 |
| Phosphorus (P) | — | 0.025 |
| Sulfur (S) | — | 0.025 |
| Silicon (Si) | 0.10 | 0.50 |
| Molybdenum (Mo) | 0.44 | 0.65 |
| Chromium (Cr) | — | — |
Composition Notes:
| Element | Engineering Note |
| Molybdenum (0.44-0.65%) | Provides solid-solution strengthening and creep resistance |
| Carbon (0.10-0.20%) | Adequate for strength and hardenability |
| No chromium | No intentional chromium addition; oxidation resistance similar to carbon steel |
Unlike other CrMo grades, T1 contains no chromium, which limits its oxidation resistance and high-temperature strength compared to T2 or T11. However, it is less expensive and perfectly suitable for applications where oxidation is not a concern.
3. Mechanical Properties
The mechanical properties of SA213 T1 are similar to carbon steel at room temperature but maintain better strength at elevated temperatures due to molybdenum.
Tensile Requirements (Room Temperature):
| Property | Minimum | Typical | Unit |
| Tensile Strength | 415 MPa (60 ksi) | 450-550 MPa | — |
| Yield Strength (0.2% offset) | 205 MPa (30 ksi) | 280-350 MPa | — |
| Elongation in 2 in. or 50 mm | 30% | 35-40% | — |
For thin walls, elongation adjustment follows same formula as other grades.
Hardness Requirements:
| Property | Maximum |
| Brinell Hardness (HBW) | 163 |
| Rockwell Hardness (HRB) | 85 |
High-Temperature Tensile Properties (Reference Values):
| Temperature (°C) | Tensile Strength (MPa) | Yield Strength (MPa) |
| 20 | 450-550 | 280-350 |
| 300 | 400-480 | 230-290 |
| 400 | 380-450 | 210-260 |
| 450 | 350-420 | 190-240 |
| 480 | 300-380 | 150-200 |
Creep Rupture Strength (Typical Values):
| Temperature (°C) | 100,000 Hour Stress (MPa) |
| 430 | 60-75 |
| 450 | 45-60 |
| 480 | 30-40 |
T1 is best suited for service up to 480°C (900°F). Above that, higher alloys are recommended.
4. Heat Treatment Requirements
T1 tubes are normally supplied in the annealed condition.
Heat Treatment Requirements:
| Condition | Process | Temperature Range | Cooling Method |
| Annealed | Full annealing | 870-900°C (1600-1650°F) | Furnace cool |
| Normalized | Normalizing | 900-930°C (1650-1700°F) | Air cool |
Manufacturer: Womic Steel provides heat treatment certificates upon request.
5. Dimensional Tolerances
Dimensional tolerances follow ASTM A213 / A1016 as described for other grades.
● OD tolerances same as T11/T22.
● WT tolerances: ±10% for cold drawn; for hot finished, same sliding scale.
● Straightness: 0.2% of length.
● Length tolerances: random 5-12 m; specific +50-100 mm / -0.
6. Available Sizes and Specifications
Same size ranges as other SA213 tubes.
Common T1 Tube Sizes (OD x WT in mm):
25.4 x 2.5, 31.8 x 3.0, 38.1 x 3.5, 44.5 x 4.0, 50.8 x 4.0, 50.8 x 5.0, 60.3 x 5.0, 63.5 x 5.0, 76.2 x 6.0, 88.9 x 6.0, 101.6 x 8.0
Manufacturer: Womic Steel maintains inventory of T1 tubes for industrial boiler and heat exchanger applications.
7. Inspection and Testing Requirements
Standard SA213 tests apply:
| Test | Requirement | Frequency |
| Chemical Analysis | Required | Per heat |
| Tensile Test | Required | Per heat |
| Hardness Test | Required | Per heat |
| Flattening Test | Required | Per lot |
| Flaring Test | Required | Per lot |
| Hydrostatic or NDT | 100% | Each tube |
8. Applications
| Industry | Application |
| Power Generation | Lower-temperature superheaters, economizers, boiler water walls (where chromium not required) |
| Industrial Boilers | Package boilers, waste heat recovery units |
| Heat Exchangers | Shell and tube exchangers for medium temperature service (up to 450°C) |
| Petrochemical | Moderate-temperature process piping |
| General Industry | High-temperature steam lines where oxidation is not a concern |
T1 is a cost-effective upgrade from carbon steel when operating temperatures exceed 400°C but the added cost of chromium is not justified. It is less common than T2 but still specified in some industrial boiler designs.
9. Comparison with Carbon Steel and T2
| Grade | Cr (%) | Mo (%) | Max Temp (°C) | Oxidation Resistance | Cost |
| Carbon Steel | 0 | 0 | 400 | Poor | Lowest |
| T1 | 0 | 0.5 | 480 | Poor | Low |
| T2 | 0.5 | 0.5 | 510 | Moderate | Low-medium |
T1 provides creep strength improvement over carbon steel without the cost of chromium, but its oxidation resistance remains similar to carbon steel, limiting its use in oxidizing atmospheres.
10. Welding Procedure for SA213 T1
T1 has excellent weldability due to its low carbon equivalent and absence of chromium.
Recommended Welding Processes: SMAW, GTAW, GMAW, SAW.
Recommended Filler Metals:
| Filler Metal | AWS Classification |
| ER70S-2 / ER70S-6 | AWS A5.18 |
| E7018 | AWS A5.1 |
Preheat: Generally not required for thin walls (t < 12 mm). For thicker sections, preheat to 100-150°C (212-302°F).
PWHT: Required by code for thickness > 19 mm (3/4 in) but often waived for tubes under 12 mm depending on service.
PWHT Temperature: 620-680°C (1150-1250°F).
11. Traceability and Marking
Each tube marked with: Manufacturer, ASTM A213/ASME SA213 T1, UNS K11596, size, heat number, length, NDT method.
Marking Example:
| Line | Content |
| Line 1 | Womic Steel ASTM A213/ASME SA213 T1 |
| Line 2 | 50.8mm x 4.0mm x 6.0m |
| Line 3 | Heat No: H12345 / UNS K11596 |
| Line 4 | ECT |
12. Quality Documents
● Mill Test Report (EN 10204 Type 3.1) – included
● Heat Treatment Certificate – included
● Hydrostatic/NDT Certificate – included
● Dimensional Inspection Report – included
● Certificate of Origin – included
● Third-Party Inspection – optional
13. Contact Information
Website: www.womicsteel.com
E-mail: sales@womicsteel.com
Tel / WhatsApp / WeChat:
Victor: +86 15575100681
Jack: +86 18390957568
Womic Steel – Your reliable partner for SA213 T1 seamless alloy tubes, stainless steel products, and custom solutions for boiler, superheater, heat exchanger, and industrial heat transfer applications.
Post time: Sep-15-2026