Premium SA213 T91 Seamless Alloy Tube for Advanced Superheaters, Reheaters, High-Pressure Boilers, and Ultra-Supercritical Power Plants
Womic Steel produces high-quality SA213 T91 Seamless Alloy Steel Tube, manufacturing chromium-molybdenum-vanadium-niobium (9Cr-1Mo-V-Nb) ferritic alloy tubes in accordance with ASTM A213 / ASME SA213 specifications. Our SA213 T91 tubes meet the demanding requirements of the American Society of Mechanical Engineers (ASME) Boiler and Pressure Vessel Code, with a minimum tensile strength of 585 MPa and exceptional creep resistance at elevated temperatures up to 650°C (1200°F). These seamless alloy tubes are the ideal choice for advanced superheaters, reheaters, high-pressure boilers, heat exchangers, and ultra-supercritical power plant applications where T22 and T9 grades cannot meet the required creep strength and oxidation resistance.
Manufacturer: Womic Steel
1. Product Definition and Scope
SA213 T91 (UNS K90901) is a seamless ferritic alloy steel tube specified under ASTM A213 / ASME SA213 for use in boilers, superheaters, heat exchangers, and other high-temperature pressure-containing equipment. The “T91″ designation indicates a modified 9Cr-1Mo steel with controlled additions of vanadium and niobium (columbium), which provide outstanding creep rupture strength significantly higher than traditional T9 or T22 grades. T91 is the standard material for ultra-supercritical boilers and advanced combined cycle power plants where operating temperatures reach 650°C.
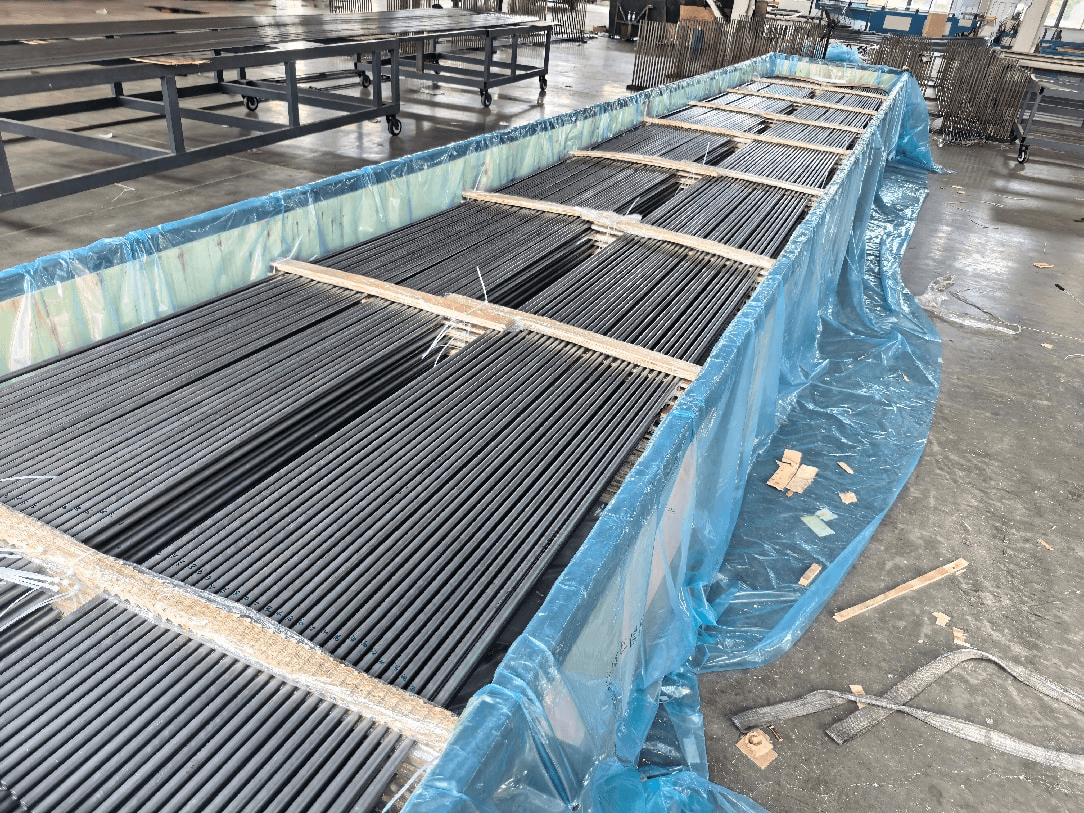
Manufacturing Process: T91 tubes shall be manufactured by the seamless process and shall be either hot-finished or cold-finished. T91 is typically supplied in the normalized and tempered condition. The normalized and tempered microstructure—tempered martensite—provides the required high-temperature strength and ductility. The addition of vanadium and niobium forms stable carbonitride precipitates that resist coarsening, delivering superior long-term creep performance.
Grade Designation:
| Designation | Meaning |
| SA213 | ASME specification for seamless ferritic and austenitic alloy-steel tubes for boilers, superheaters, and heat exchangers |
| T91 | Grade designation: 9% Chromium – 1% Molybdenum with Vanadium and Niobium |
| UNS K90901 | Unified numbering system designation for T91 |
Equivalent Standards and Grades:
| Standard | Equivalent Grade |
| ASTM A213 / ASME SA213 | T91 |
| EN 10216-2 | X10CrMoVNb9-1 (1.4903) |
| DIN 17175 | X10CrMoVNb9-1 |
| JIS G3462 | STBA 28 / STBA 29 |
| BS 3059 | 622-490 |
Manufacturer: Womic Steel
2. Chemical Composition Requirements
The chemical composition of SA213 T91 is carefully balanced with microalloying elements (vanadium and niobium) to achieve a stable tempered martensitic microstructure with fine carbonitride precipitation for excellent creep strength.
SA213 T91 Chemical Composition (Heat Analysis – Seamless Tube):
| Element | Composition (%) – Minimum | Composition (%) – Maximum |
| Carbon (C) | 0.08 | 0.12 |
| Manganese (Mn) | 0.30 | 0.60 |
| Phosphorus (P) | — | 0.020 |
| Sulfur (S) | — | 0.010 |
| Silicon (Si) | 0.20 | 0.50 |
| Chromium (Cr) | 8.00 | 9.50 |
| Molybdenum (Mo) | 0.85 | 1.05 |
| Vanadium (V) | 0.18 | 0.25 |
| Niobium (Nb) | 0.06 | 0.10 |
| Nitrogen (N) | 0.030 | 0.070 |
| Aluminum (Al) | — | 0.040 |
| Nickel (Ni) | — | 0.40 |
Composition Notes:
● The combination of vanadium (0.18-0.25%) and niobium (0.06-0.10%) forms fine MX-type carbonitrides that pin grain boundaries and dislocations, providing exceptional creep resistance.
● Nitrogen (0.030-0.070%) is intentionally added to promote nitride precipitation and strengthen the matrix.
● Low sulfur (≤0.010%) and phosphorus (≤0.020%) improve toughness and weldability.
● The controlled carbon range (0.08-0.12%) ensures hardenability for martensite formation without excessive hardness.
Compared to T9, T91 offers roughly double the creep-rupture strength at 600°C and significantly better oxidation resistance, allowing designers to reduce wall thickness or increase service temperature.
3. Mechanical Properties
The mechanical properties of SA213 T91 seamless tubes are significantly higher than lower-alloy CrMo grades, enabling thinner walls and higher operating pressures.
Tensile Requirements (Room Temperature):
| Property | Minimum | Typical | Unit |
| Tensile Strength | 585 MPa (85 ksi) | 650-750 MPa | — |
| Yield Strength (0.2% offset) | 415 MPa (60 ksi) | 500-600 MPa | — |
| Elongation in 2 in. or 50 mm | 20% | 25-30% | — |
For thin-wall tubes, elongation adjustments follow the same principles as other grades, but the minimum values are adjusted per ASTM A213.
Hardness Requirements:
| Property | Maximum |
| Brinell Hardness (HBW) | 250 |
| Rockwell Hardness (HRC) | 25 (typical) |
High-Temperature Tensile Properties (Reference Values):
● At 600°C, yield strength remains above 300 MPa, significantly higher than T22.
● At 650°C, T91 still retains useful strength where T22 would have little creep resistance.
Creep Rupture Strength (Typical Values – the key advantage of T91):
| Temperature (°C) | 100,000 Hour Stress (MPa) |
| 550 | 140-160 |
| 600 | 85-100 |
| 650 | 45-55 |
| 700 | 20-25 |
The creep strength of T91 at 600°C is approximately 2-3 times that of T22 and 1.5-2 times that of T9, making it the material of choice for supercritical and ultra-supercritical boiler components.
4. Heat Treatment Requirements
T91 tubes are always supplied in the normalized and tempered condition to develop the required tempered martensitic structure.
Heat Treatment Requirements:
| Condition | Temperature Range | Cooling Method | Purpose |
| Normalizing | 1040-1080°C (1900-1975°F) | Air or accelerated cooling | Austenitize, dissolve carbides |
| Tempering | 730-780°C (1350-1440°F) | Air | Transform to tempered martensite |
Important Notes:
● The normalizing temperature is higher than for T9/T22 to fully dissolve vanadium and niobium carbonitrides.
● Tempering below the lower critical temperature develops the stable tempered martensite microstructure.
● Post-weld heat treatment (PWHT) is mandatory for T91; typical PWHT temperature is 730-760°C (1350-1400°F) with controlled cooling.
Manufacturer: Womic Steel provides full heat treatment certificates including time-temperature charts for each heat.
5. Dimensional Tolerances
T91 tubes can be supplied as hot-finished or cold-drawn. Tolerances follow ASTM A213 / A1016.
Cold Drawn Tubes (most common for T91):
| OD Range (mm) | OD Tolerance (mm) | Wall Thickness Tolerance |
| OD < 25.4 | ±0.10 | ±10% |
| 25.4 – 38.1 | ±0.15 | ±10% |
| 38.1 – 50.8 | ±0.20 | ±10% |
| 50.8 – 63.5 | ±0.25 | ±10% |
| 63.5 – 76.2 | ±0.30 | ±10% |
| 76.2 – 101.6 | ±0.38 | ±10% |
| 101.6 – 190.5 | +0.38 / -0.64 | ±10% |
Straightness: 0.2% of total length (2 mm per meter). Length tolerances: same as other grades (random 5-12 m, specific lengths with +50-100 mm / -0).
6. Available Sizes and Specifications
T91 is most commonly supplied in cold-drawn condition for smaller diameters (superheater and reheater tubes) and hot-finished for larger headers.
Typical Size Range:
OD: 12.7 mm (1/2″) up to 101.6 mm (4″) for cold-drawn; up to 219.1 mm (8-5/8″) for hot-finished.
WT: 1.6 mm to 15.0 mm depending on application.
Common T91 Tube Sizes (OD x WT in mm):
31.8 x 3.0, 38.1 x 4.0, 44.5 x 5.0, 50.8 x 5.0, 50.8 x 6.0, 60.3 x 6.0, 63.5 x 6.0, 76.2 x 8.0, 88.9 x 8.0, 101.6 x 10.0.
U-Bend Tubes: Available with controlled bending radius and post-bend heat treatment (stress relief).
Manufacturer: Womic Steel maintains a dedicated inventory of T91 tubes for power generation projects.
7. Inspection and Testing Requirements
T91 tubes require the same basic tests as other SA213 grades (chemical, tensile, hardness, flattening, flaring). However, due to the critical nature of T91 in high-temperature service, additional testing is often specified.
| Test | Requirement | Frequency |
| Chemical Analysis | Required | Per heat |
| Tensile Test (RT) | Required | Per heat |
| High-Temperature Tensile (optional) | Upon request | Per heat |
| Hardness Test | Required | Per heat |
| Flattening / Flaring | Required | Per lot |
| Hydrostatic or NDT (ECT/UT) | 100% | Each tube |
| Charpy Impact Test (optional) | Upon request | Per heat |
| Microstructure Examination | Upon request | Per heat |
| Creep Rupture Test (optional) | Upon request | Special order |
Hardness Control: Maximum 250 HBW. T91 is sensitive to overheating during welding, so hardness testing of welds and HAZ is often required.
NDT: 100% eddy current or ultrasonic testing is standard. For critical applications, both hydrostatic and UT may be required.
8. Applications
SA213 T91 seamless tubes are specifically designed for advanced high-efficiency power plants and other high-temperature services.
| Industry | Application |
| Ultra-Supercritical Power Plants | High-temperature superheater and reheater sections operating up to 650°C |
| Supercritical Power Plants | Final stage superheaters and reheaters |
| Combined Cycle HRSGs | High-temperature sections where gas turbine exhaust exceeds 600°C |
| Biomass and Waste-to-Energy | High-temperature corrosion-resistant superheater tubes |
| Petrochemical | High-temperature hydrogen service (hydrocracker / hydrotreater) |
| Refining | High-temperature furnace coils and transfer lines |
T91 enables higher steam temperatures (up to 600-620°C) and pressures, leading to improved thermal efficiency and reduced CO₂ emissions. It is now the standard material for modern supercritical boiler final superheater sections.
9. Comparison with T22 and T9
| Grade | Cr (%) | Mo (%) | V+Nb | Min YS (MPa) | Max Temp (°C) | Creep Strength at 600°C (100kh) |
| T22 | 2.25 | 1.0 | No | 205 | 565 | ~35 MPa |
| T9 | 9 | 1.0 | No | 205 | 593 | ~50 MPa |
| T91 | 9 | 1.0 | Yes | 415 | 650 | ~90 MPa |
T91 provides roughly double the creep strength of T9 at 600°C, allowing designers to use thinner walls or increase operating temperature by 30-50°C.
10. Welding Procedure for SA213 T91
T91 has high hardenability and requires strict welding procedures to avoid cracking and to restore the tempered martensite structure.
Recommended Welding Processes: GTAW (TIG) for root pass (preferred), SMAW with low-hydrogen electrodes for fill and cap, GMAW (short-circuit transfer) for mechanized welding.
Recommended Filler Metals:
| Filler Metal | AWS Classification | Application |
| ER90S-B9 | AWS A5.28 (matching) | GTAW root |
| E9015-B9 | AWS A5.5 (matching) | SMAW fill |
| ERNiCr-3 | AWS A5.14 (alternative) | When dissimilar welding to stainless |
Critical Welding Requirements:
● Preheat: 150-250°C (300-480°F) – mandatory for all thicknesses.
● Maximum Interpass Temperature: 300°C (572°F).
● Post-Weld Heat Treatment (PWHT): 730-760°C (1350-1400°F) – mandatory.
● PWHT Hold Time: Minimum 1 hour per 25mm thickness, but typically 2-4 hours for tube welding.
● Hydrogen Control: Low-hydrogen consumables (H8 or lower) and proper storage are essential.
● Back Purging: Argon purge for root pass to prevent oxidation.
PWHT must be performed to temper the hard martensitic weld metal and HAZ, restoring ductility and creep strength. Delayed hydrogen cracking is a risk if proper preheat and PWHT are not followed.
11. Traceability and Marking
Each tube is stencil marked with:
● Manufacturer name (Womic Steel)
● Specification (ASTM A213 / ASME SA213 T91)
● UNS K90901
● Size (OD x WT)
● Heat number
● Length
● NDT method (ECT/UT/Hydro)
Marking Example:
| Line | Content |
| Line 1 | Womic Steel ASTM A213/ASME SA213 T91 |
| Line 2 | 50.8mm x 5.0mm x 6.0m |
| Line 3 | Heat No: H12345 / UNS K90901 |
| Line 4 | UT / Hydro |
12. Quality Documents (Standard for T91 shipments)
● Mill Test Report (EN 10204 Type 3.1) with full chemical analysis and mechanical properties.
● Heat Treatment Certificate (normalizing and tempering curves).
● Hydrostatic Test Report (or NDT certificate).
● Dimensional Inspection Report.
● Certificate of Origin.
● Third-Party Inspection (SGS, BV, DNV, TUV, LR, ABS) – optional.
For critical orders, Charpy impact test results, creep rupture data, and microstructure photos can be provided upon request.
13. Contact Information
Website: www.womicsteel.com
E-mail: sales@womicsteel.com
Tel / WhatsApp / WeChat:
Victor: +86 15575100681
Jack: +86 18390957568
Womic Steel – Your reliable partner for SA213 T91 seamless alloy tubes, stainless steel products, and custom solutions for advanced boiler, superheater, heat exchanger, and ultra-supercritical power generation applications.
Post time: Oct-25-2026